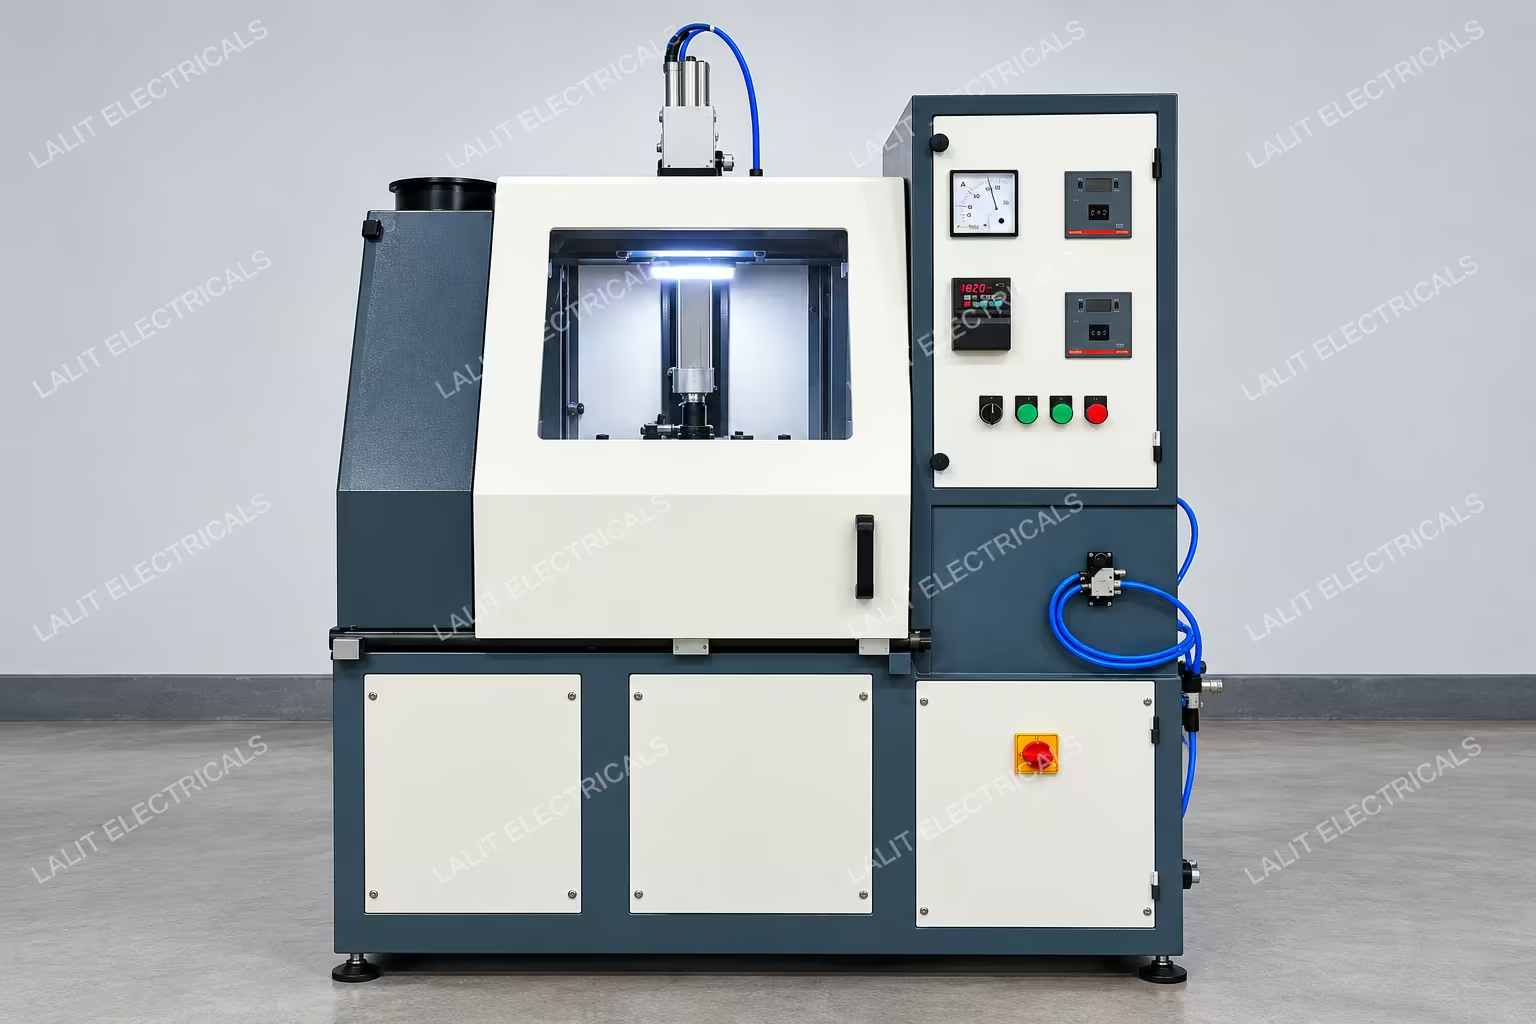
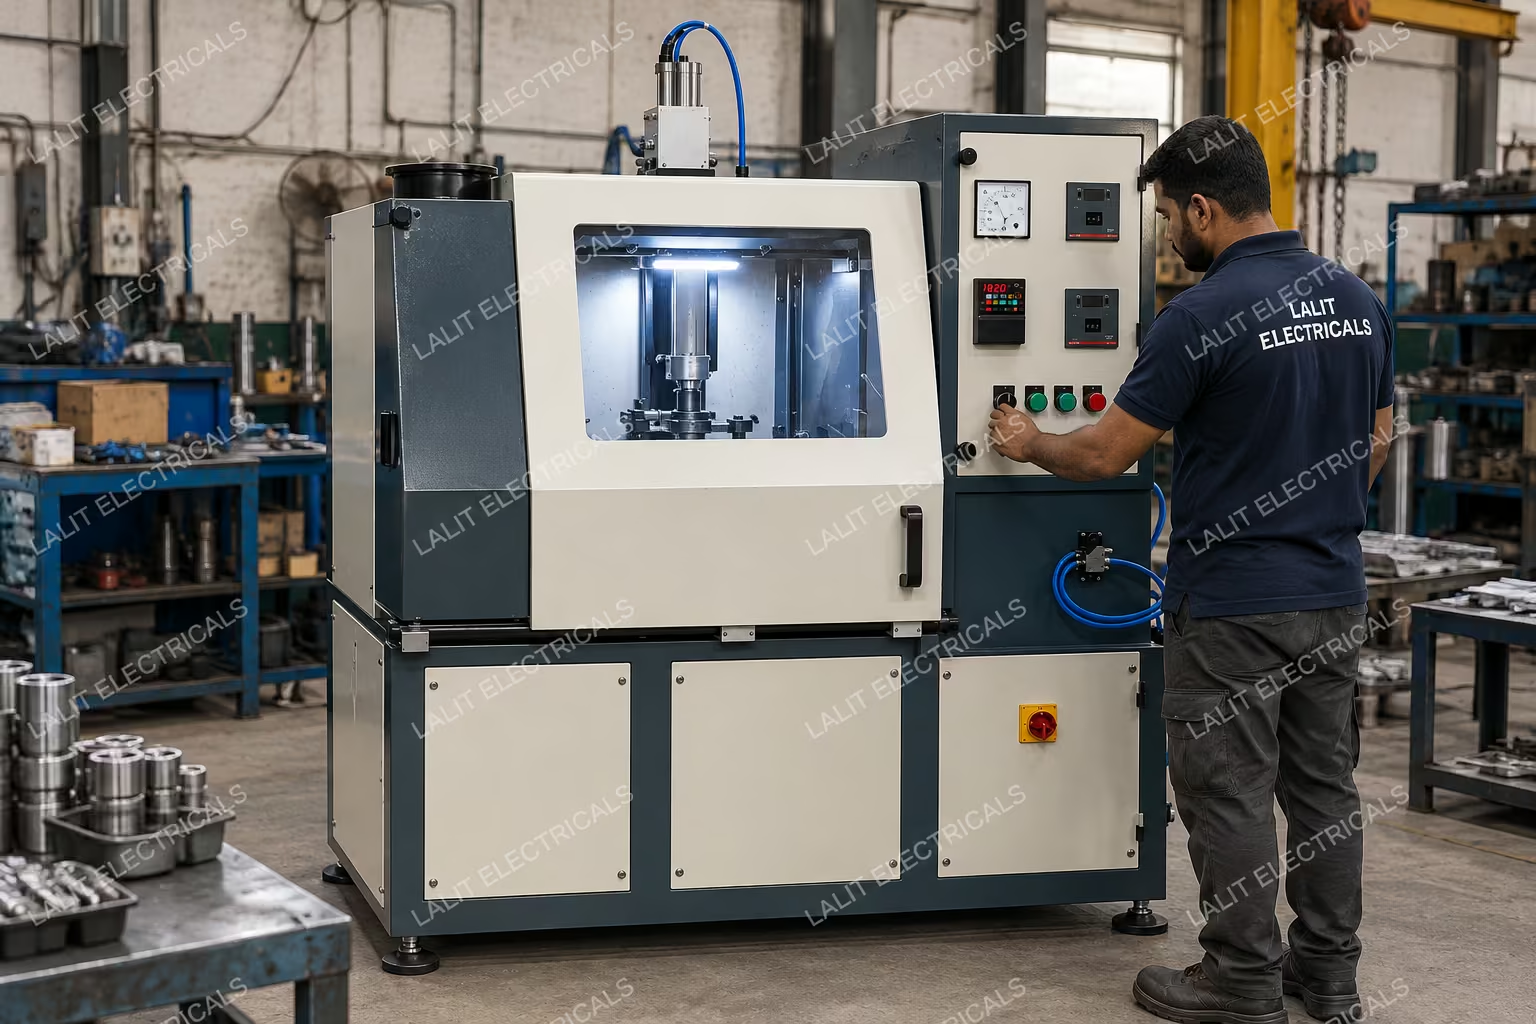
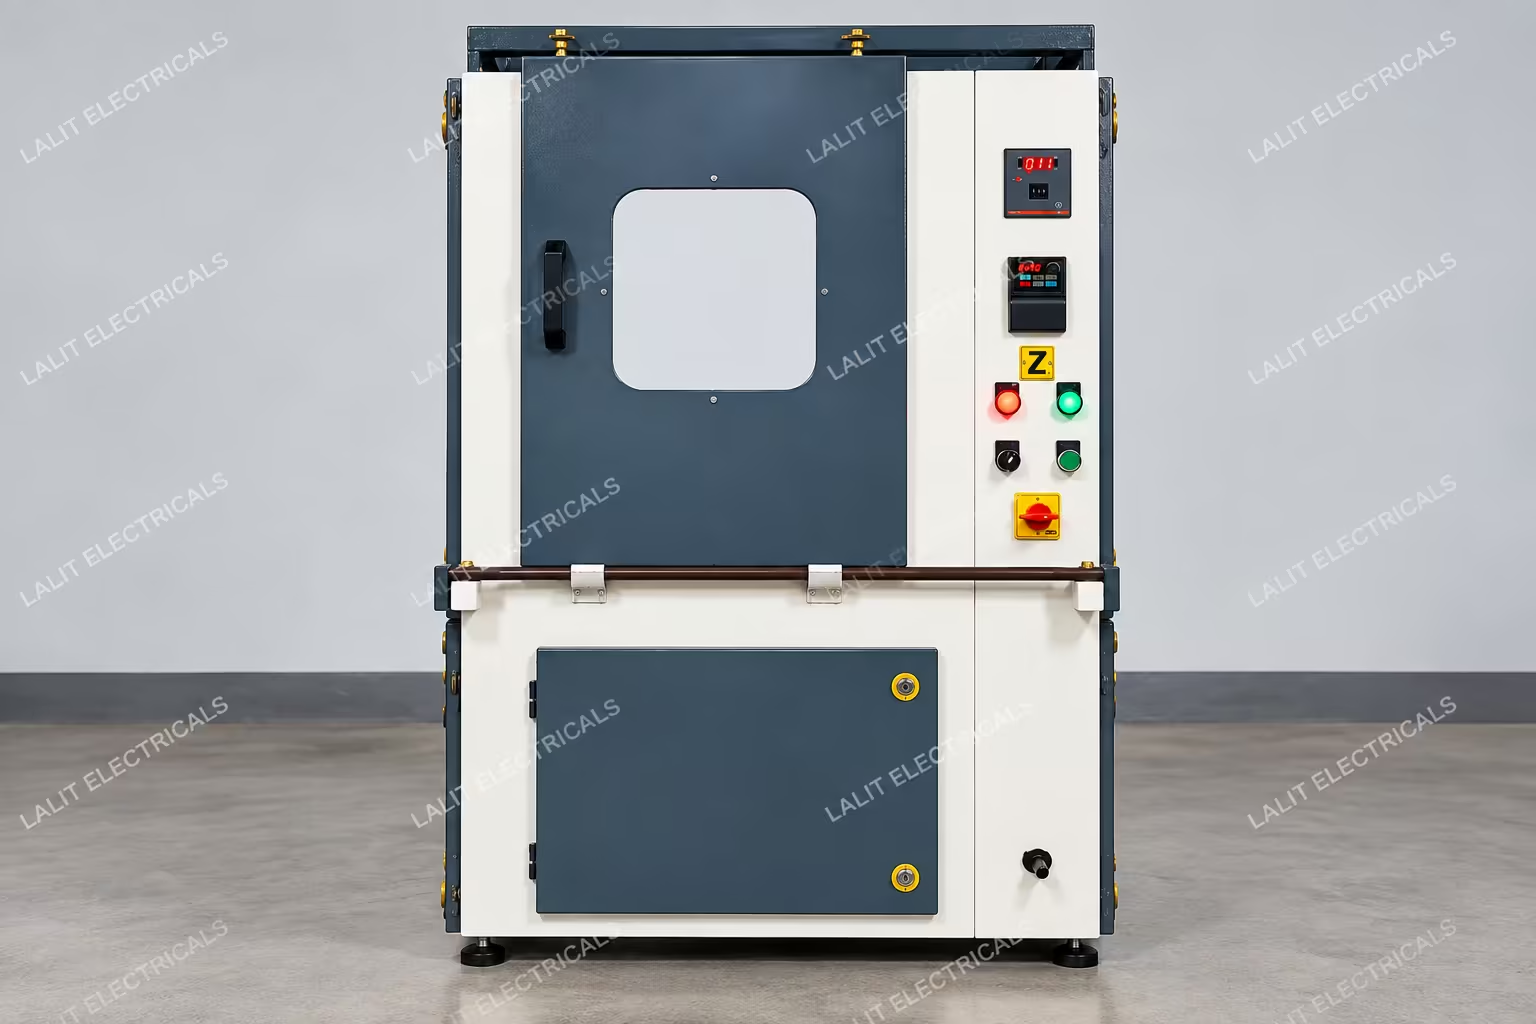
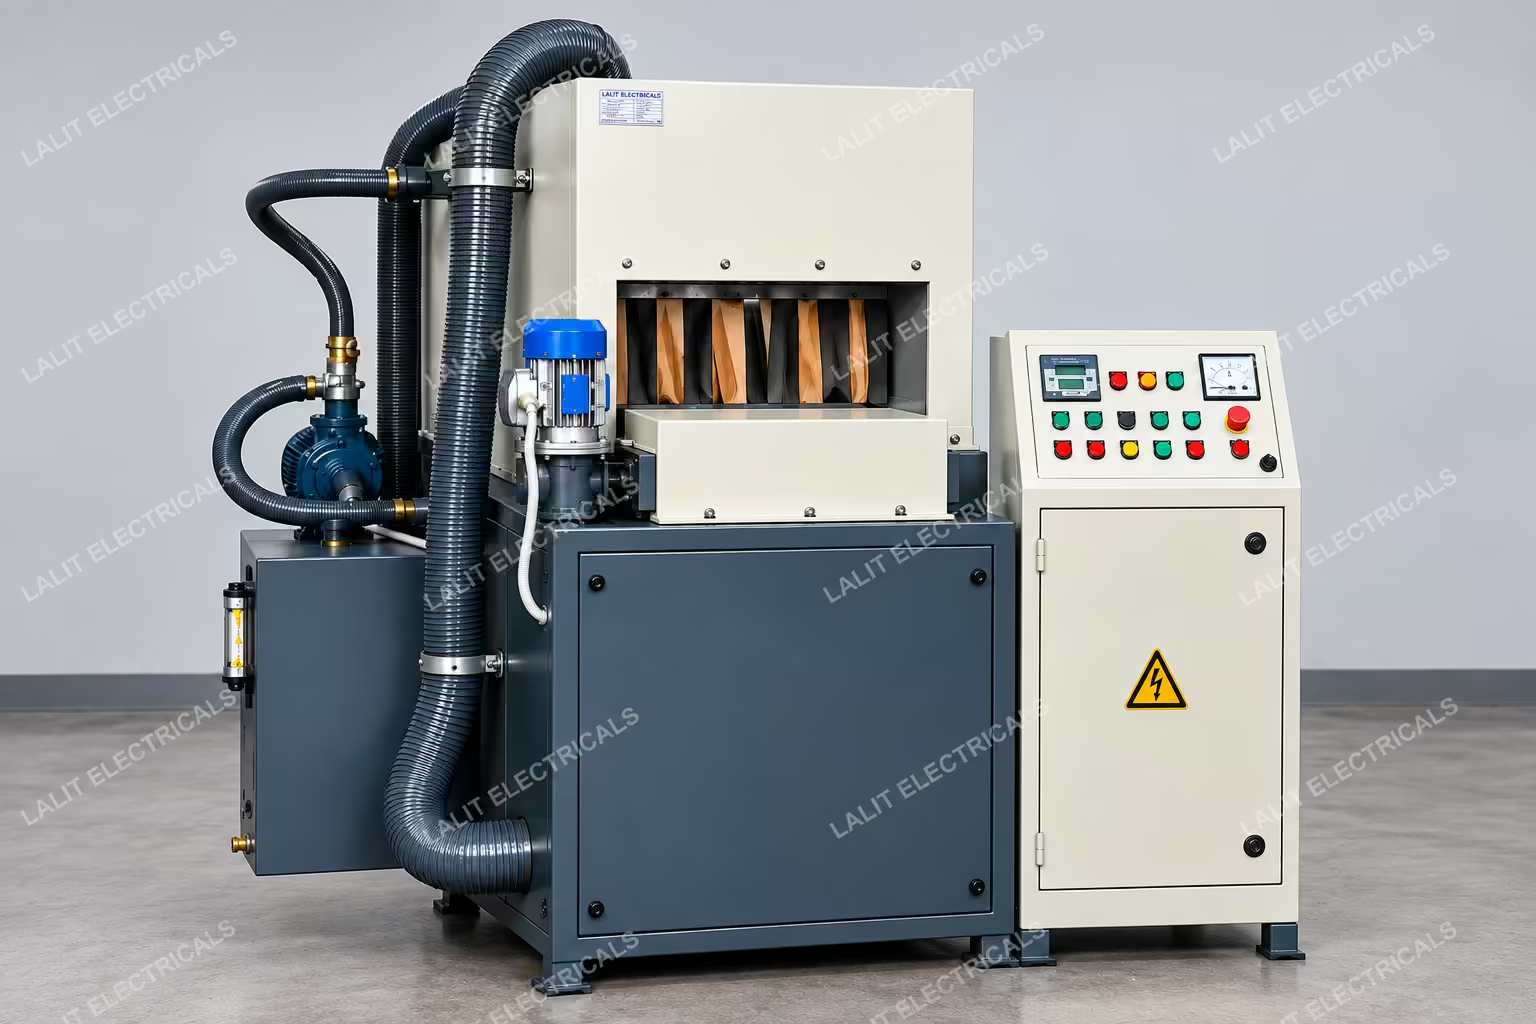
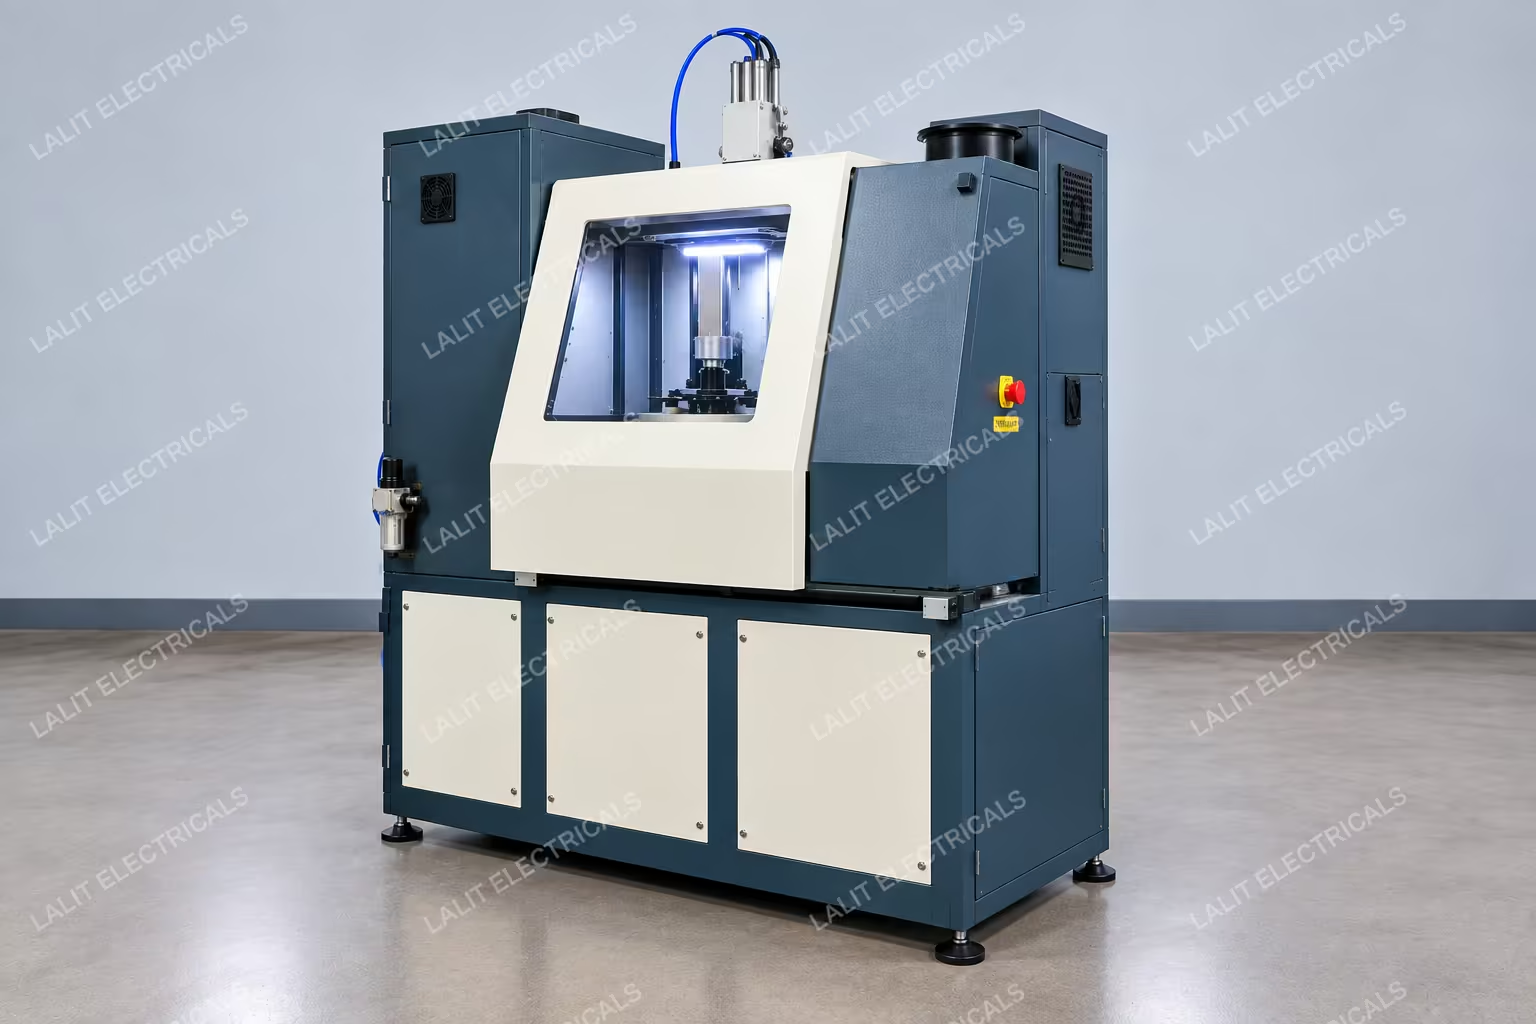
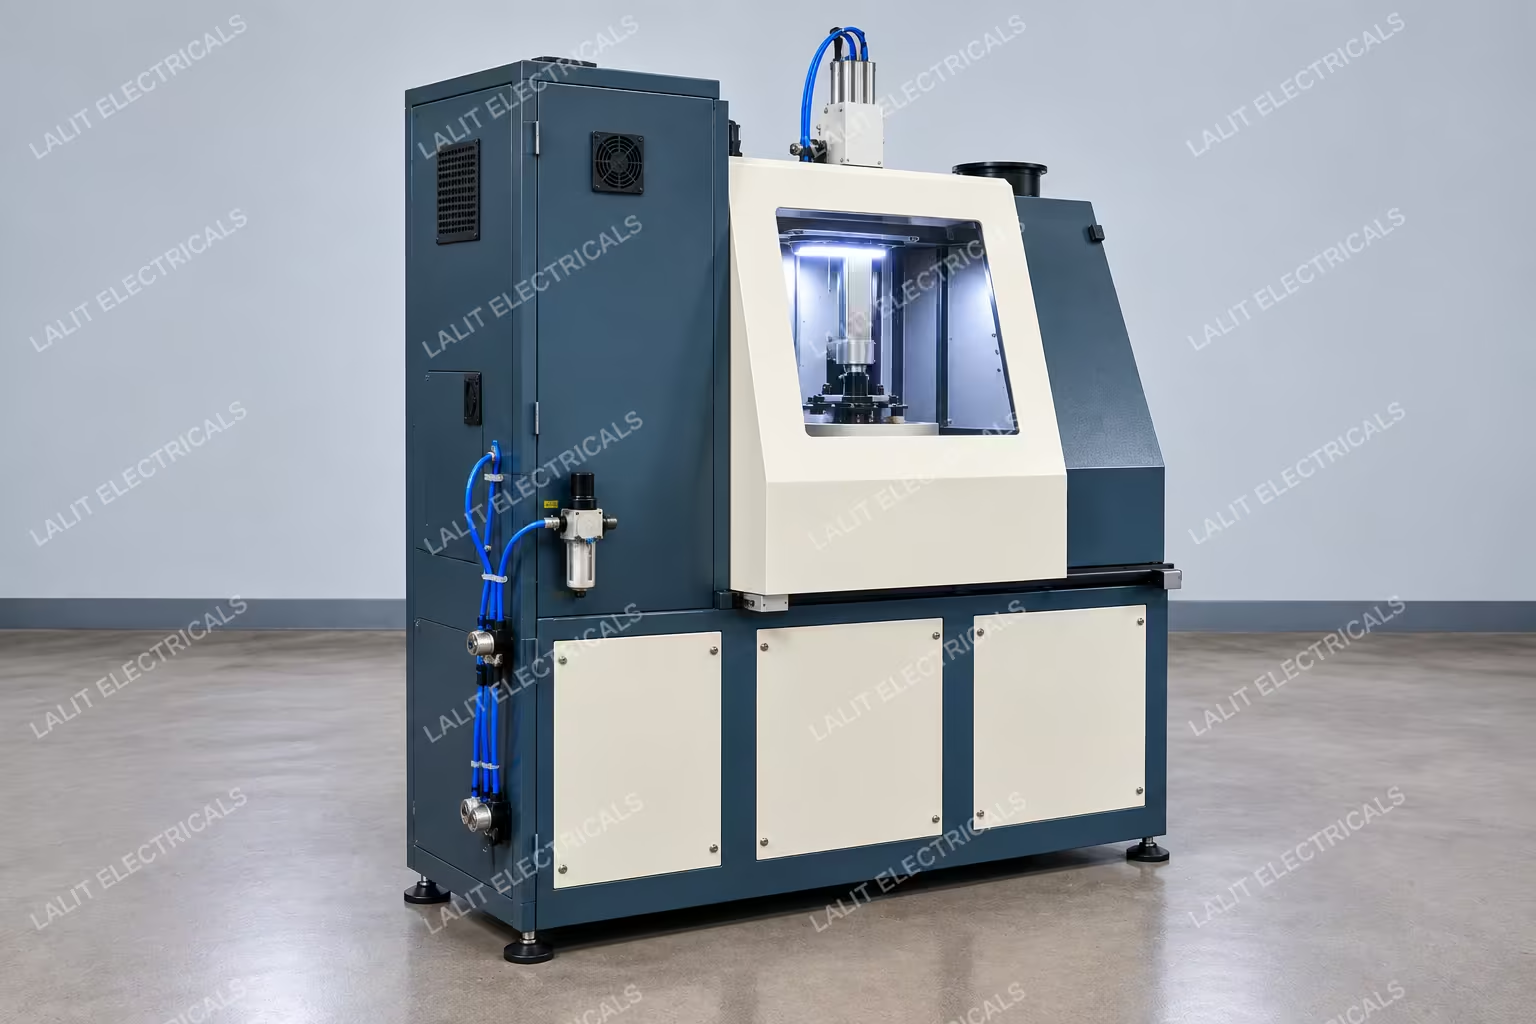
Heavy-duty spindle lapping that removes the high points which appear on gear teeth after hardening. All motions are controlled from the panel, with variable spindle speed in both forward and reverse, and the machine is modified to suit your gear.
Spindle
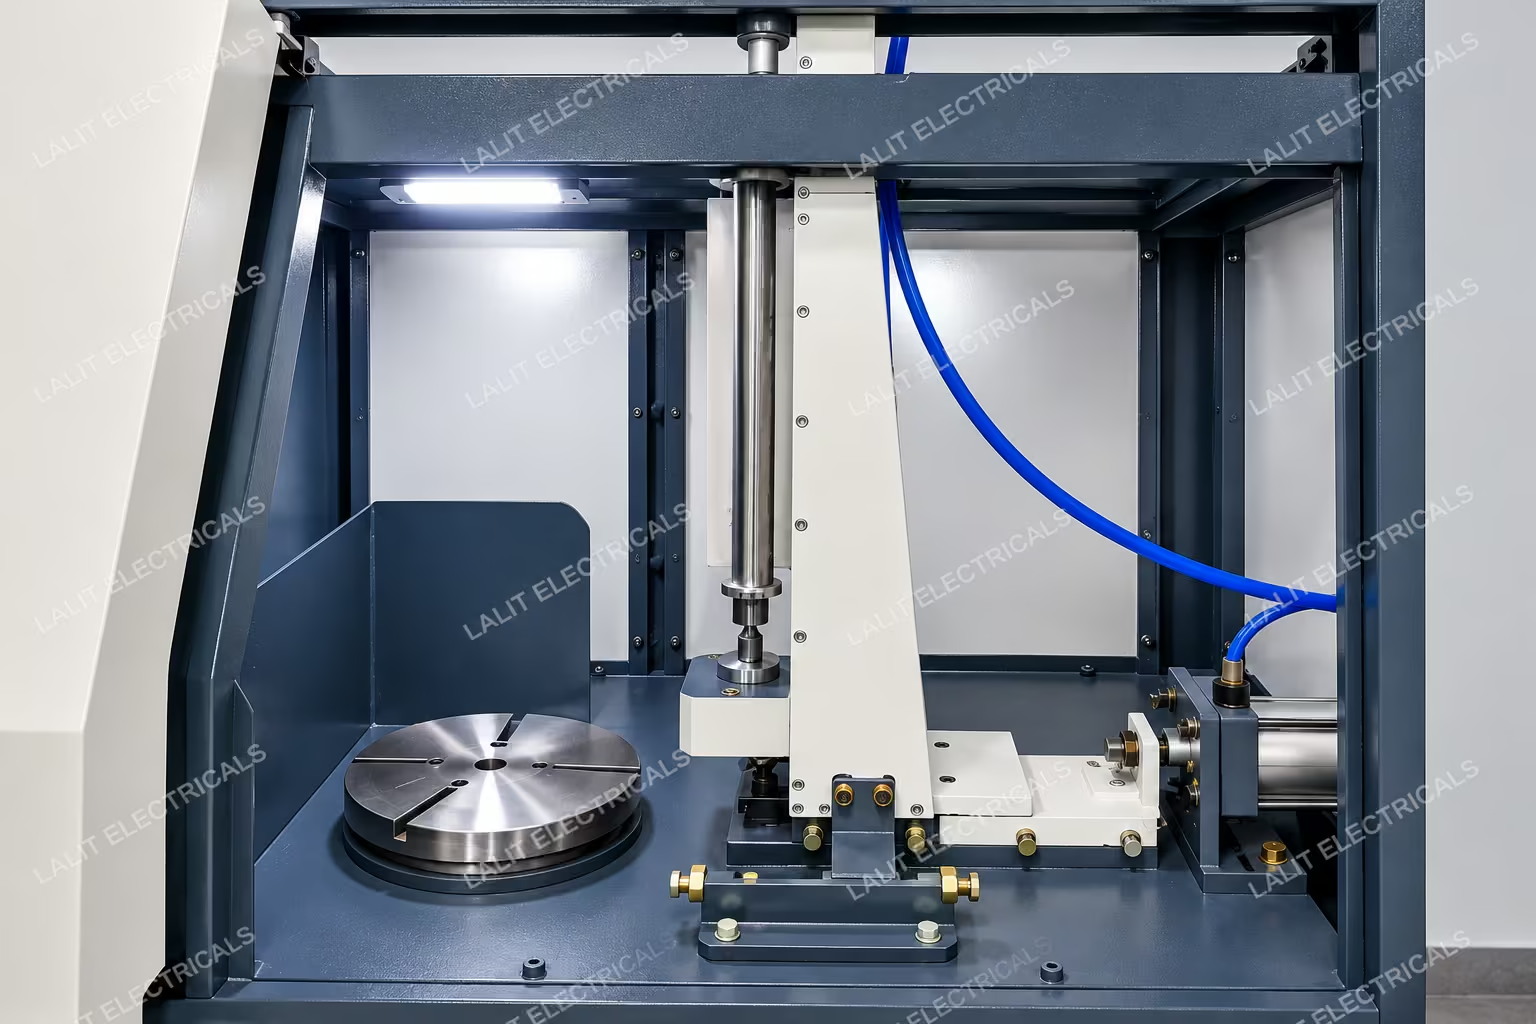
Heavy-duty lapping spindle, vertical mounting
Speed control
Variable, with forward and reverse motion
Automation
All systems controlled from the electrical control panel
Lapping medium
Compound-fed lapping gear or abrasive tooling
Fixturing
Component-specific mandrel or chuck arrangement
Customisation
Built around your gear diameter, module and cycle time
Heat treatment gives a gear the hardness it needs, but it also distorts the tooth form. Microscopic high points appear on the flanks, and those points carry the entire contact load when the gear first meshes.
Lapping removes exactly those high points, restoring the contact pattern across the full flank. The result is quieter running, better load distribution and a gear that does not wear itself in at the customer’s cost.
Our Offerings & Technology
How we build the machine
Heavy-duty spindle assembly sized for the load your gear presents
Variable speed drive with forward and reverse motion for controlled lapping cycles
Full panel control of spindle, feed and cycle timing
Component-specific mandrels, chucks and locating fixtures
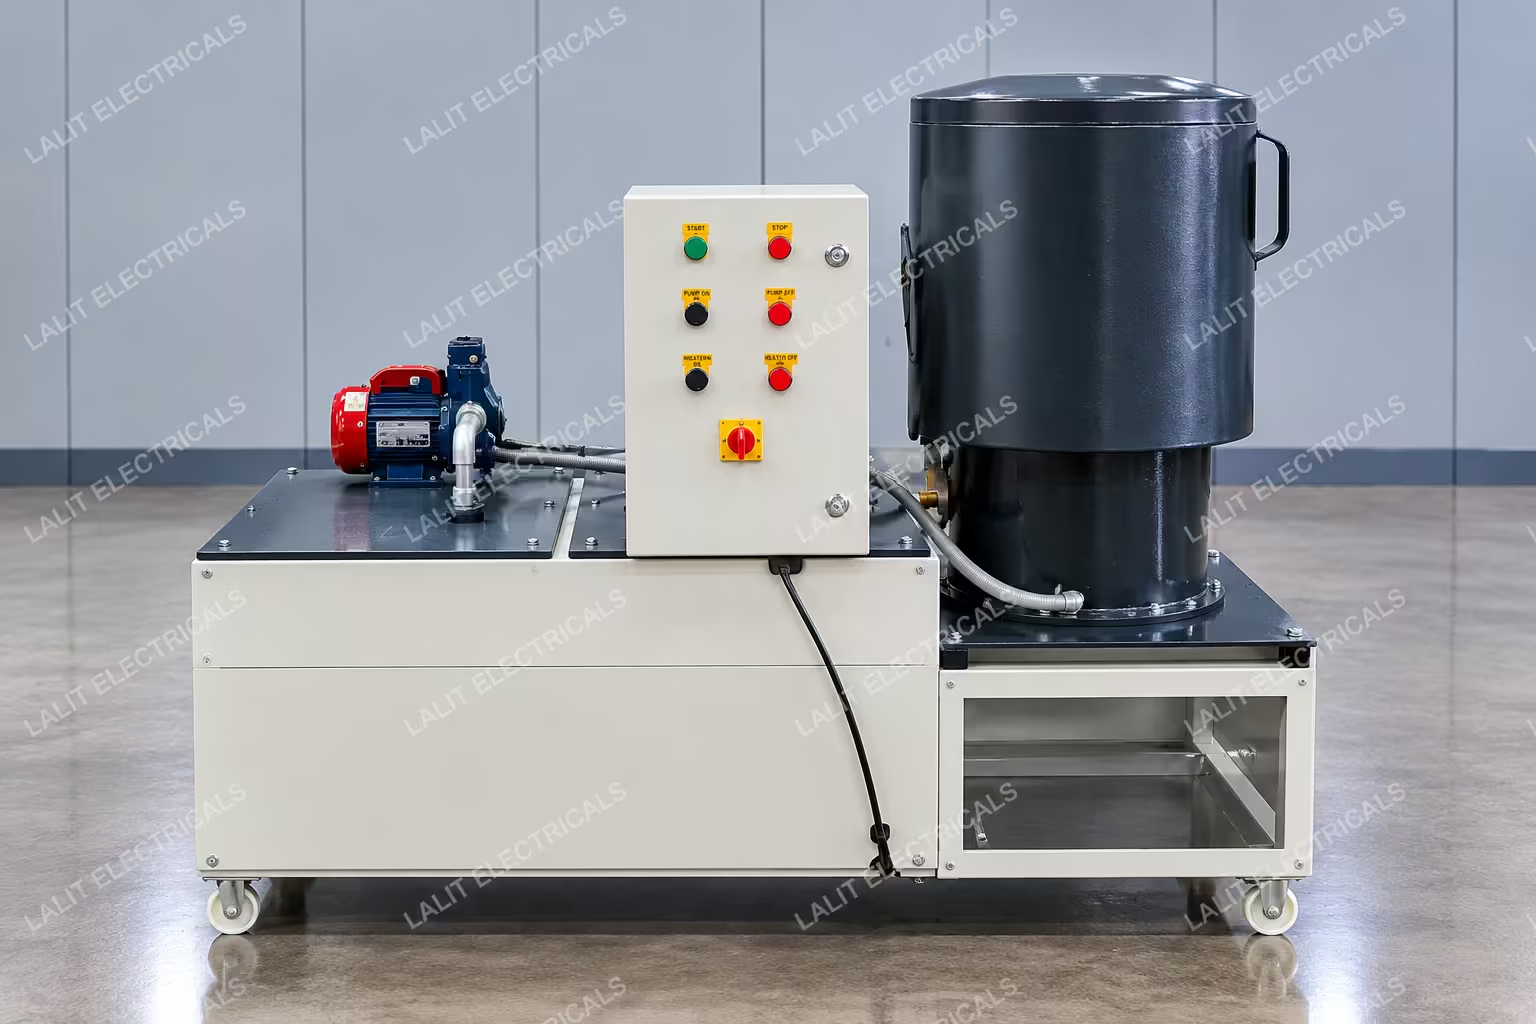
Compound feed and recovery arrangement to keep the lapping medium clean
Enclosure and tray design that keeps compound off the floor
Key Features & Advantages
Built for repeatable tooth geometry
01
Rigid spindle
A heavy-duty spindle assembly keeps the lap running true, so correction is even across the whole flank.
02
Bi-directional lapping
Forward and reverse motion works both tooth flanks evenly instead of loading one side.
03
Panel controlled
Speed, direction and cycle time are all set and repeated from the control panel, not by operator judgement.
04
Restores contact pattern
High points come off, the contact band spreads across the flank, and gear noise drops measurably.
05
Component specific
Fixturing is built around your gear rather than adapted from a standard holder.
06
Serviceable
Standard bought-out drives and bearings, with spares held and supplied from Faridabad.
Technical Specifications
Standard build
Machine type
Gear lapping machine, vertical heavy-duty spindle
Purpose
Removal of post-hardening high points on gear teeth
Spindle drive
Motor rating — to be confirmed per model
Speed control
Variable frequency drive, forward and reverse
Motion control
Fully automatic cycling through the control panel
Lapping medium
Lapping compound with mating lap gear or abrasive tool
Fixturing
Component-specific mandrel or chuck
Component capacity
Max gear diameter and module — to be confirmed
Cycle time
Set per component — to be confirmed
Automation
Control panel with timer, counter and cycle interlocks
Enclosure
Sheet metal cabinet with compound containment tray
Power supply
To be confirmed per model
Machine dimensions
To be confirmed per model
Customisation
Spindle, fixture and cycle built around your gear
Where It Is Used
Typical applications
Transmission gears
Post-hardening correction on gearbox and axle gears before assembly.
Heat treatment shops
In-house finishing of gears that have just come out of the furnace.
Machine tool builders
Spindle and drive gears that must run quiet at high speed.
Aerospace gearing
Critical gears where contact pattern is inspected and recorded.